Call us now :
 Send Inquiry

 Send Inquiry
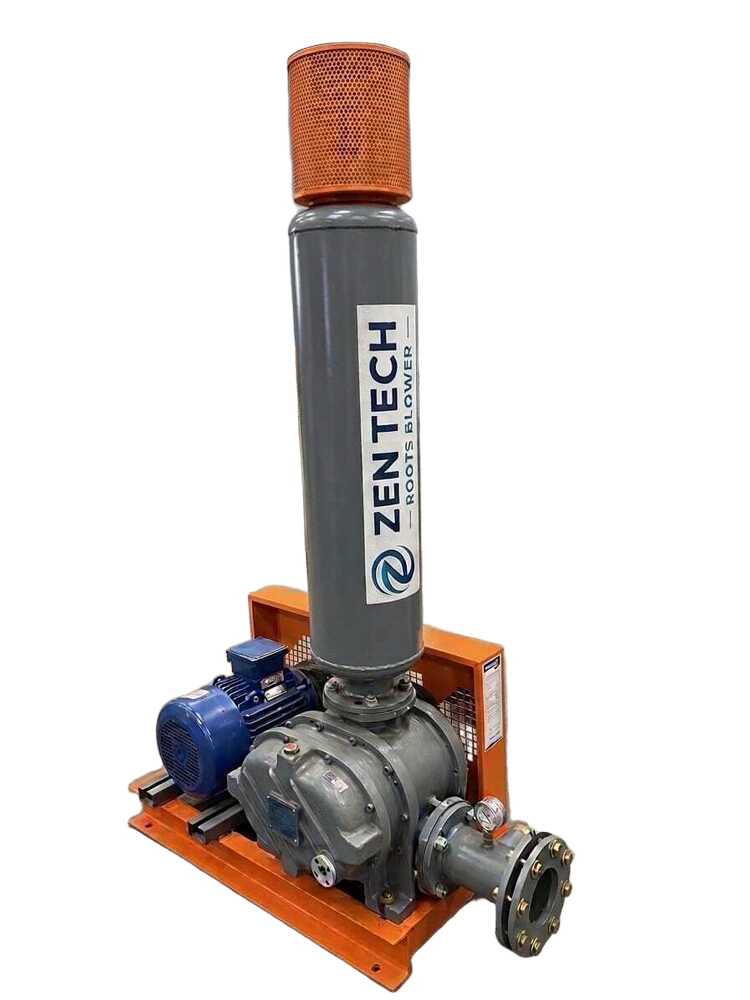
Twin Lobe Air Blower
Price 42000 INR/ Unit
MOQ : 1 Unit
Twin Lobe Air Blower Specification
- Output Power
- Custom as per model (typically 3-37 kW)
- Motor Power
- 0.75 kW to 37 kW
- Vaccum Range
- Up to 500 mm Hg (Vacuum models only)
- Flow Rate
- Maximum 5000 m3/hr
- Max Pressure
- 1 kg/cm2
- Power
- 3 HP to 50 HP
- Pressure Range
- 0 to 1 Kg/cm2
- Life Span
- 10-15 Years (With Proper Maintenance)
- Product Type
- Positive Displacement Blower
- Material
- Cast Iron/CI or Alloy Steel
- Capacity
- 50 to 5000 m3/hr
- Pressure
- Max. up to 1 kg/cm2 (0.1 MPa)
- Application
- Aeration, Pneumatic conveying, Wastewater treatment, Cement, Chemical industry
- Frequency (MHz)
- 50/60 Hz
- Motor Speed
- 1440 RPM
- Noise Level
- < 85 dB(A)
- Power Source
- Electric Motor Driven
- Voltage
- 220-415 V
- Weight
- Approx. 60-200 kg (Model dependent)
- Dimension (L*W*H)
- Custom sizes, typically 800 x 450 x 600 mm
- Color
- Black/Grey with Orange Cap
- Suction Type
- Horizontal Suction & Discharge
- Number of Lobes
- Twin Lobe (2 Lobes)
- Lubrication Type
- Splash Lubricated
- Oiling System
- Double Side Oil Chamber
- Serviceability
- Easy Servicing and Maintenance
- Drive Type
- Belt Driven/Coupled Driven
- Mounting
- Skid/Frame Mounted
- Discharge Size
- DN50-DN300 (2'' to 12'')
- Operation Mode
- Continuous Duty
- Sealing Type
- Labyrinth Seal/Mechanical Seal (Optional)
- Vibration
- Low Vibration Design
- Cooling Method
- Air Cooled
Twin Lobe Air Blower Trade Information
- Minimum Order Quantity
- 1 Unit
- Payment Terms
- Cash in Advance (CID)
- Supply Ability
- 100 Units Per Month
- Delivery Time
- 5-7 Days
- Main Domestic Market
- All India
About Twin Lobe Air Blower
Redeem an ineffable deal on our lustrous Twin Lobe Air Blower, engineered for matchless efficiency in industrial applications. Take advantage of an exclusive price cut and elevate your processes with robust features including belt or coupled drive, air-cooled operation, and splash lubrication. Designed for continuous duty, it boasts double-side oil chambers, low vibration, easy maintenance, and customizable flow rates up to 5000 m3/hr. Built from durable cast iron or alloy steel, this electric motor-driven powerhouse is ideal for aeration, wastewater, cement, and chemical industries. Avail the offer to experience top-tier performance and longevity.
Twin Lobe Air Blower: Versatile Applications and Prime Advantages
The Twin Lobe Air Blower is extensively used for aeration, pneumatic conveying, and wastewater treatment, making it integral to industries like cement and chemicals. Manufacturers and service providers alike rely on its continuous duty operation and low vibration performance. With splash lubricated, air-cooled design and simple serviceability, this equipment offers a distinct advantage: maximized output and minimal downtime, guaranteeing reliability and efficiency under diverse operating conditions.
Certifications, Delivery, and Export Markets
Certified for quality and safety, the Twin Lobe Air Blower is offered at a competitive rate. Shipped promptly to clients across India, it serves both the domestic and export market with rapid delivery times. Renowned manufacturers and suppliers ensure that each unit meets stringent standards, making it a trusted choice in major industrial sectors. Fast order processing guarantees timely deployment of your blower, reinforcing our commitment to service excellence.
FAQ's of Twin Lobe Air Blower:
Q: How does the Twin Lobe Air Blower enhance industrial applications?
A: The Twin Lobe Air Blower provides a matchless flow rate and reliable performance, making it essential for processes like aeration, pneumatic conveying, and wastewater treatment. Its continuous duty mode ensures efficiency in demanding environments.Q: What specific industries use the Twin Lobe Air Blower?
A: Industries such as cement, chemical, wastewater treatment, and those requiring pneumatic conveying rely on this blower for efficient and consistent air movement.Q: When should maintenance be performed for optimal performance?
A: Regular maintenance, typically as per the manufacturer's guidelines, ensures smooth operation and extends the blower's lifespan to 10-15 years. Easy servicing and accessible components make maintenance straightforward.Q: Where are these air blowers shipped or installed?
A: The Twin Lobe Air Blower is shipped across India and is available for export markets. Installations are customized to site requirements, and clients receive tailored units for their specific operational setups.Q: What are the benefits of choosing this Twin Lobe Air Blower model?
A: This model offers low vibration, easy maintenance, robust construction, customizable sizing, and versatile operation with various sealing and mounting options, yielding maximized efficiency and long service life.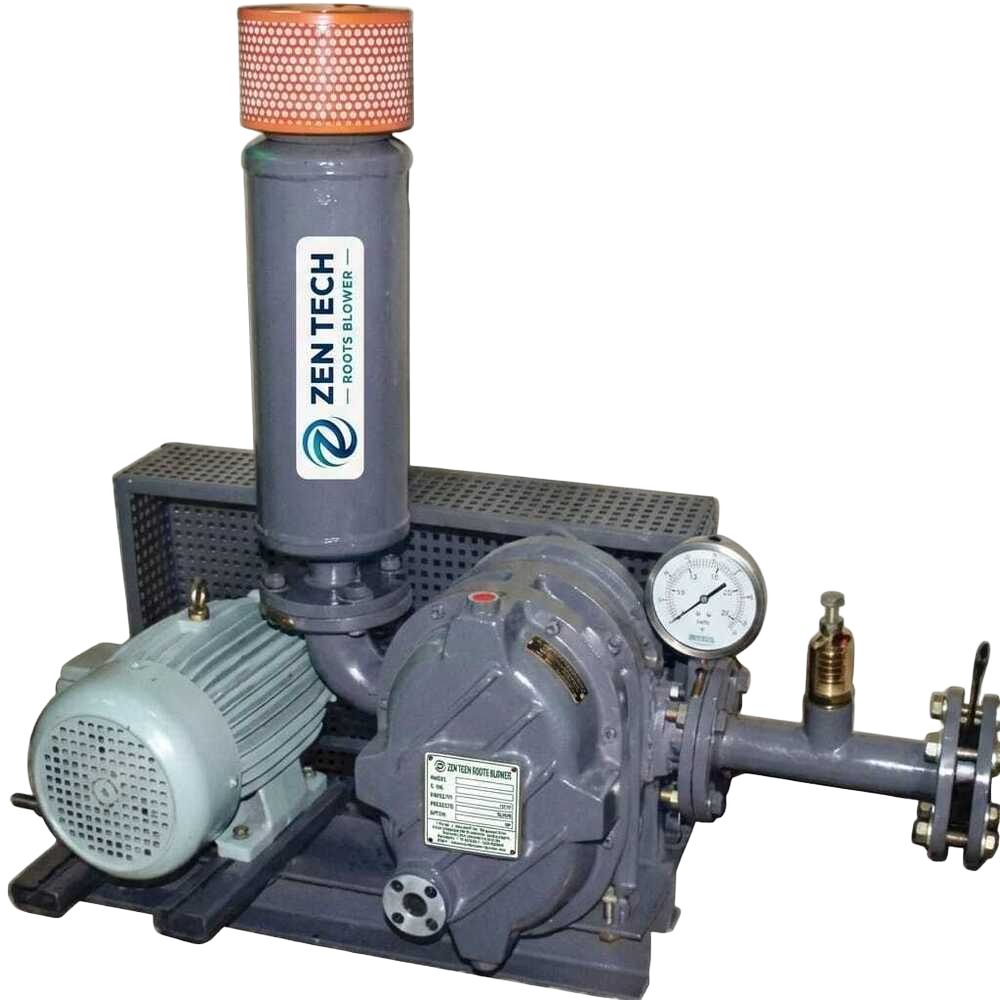
More Products in Roots Lobe Blower Category
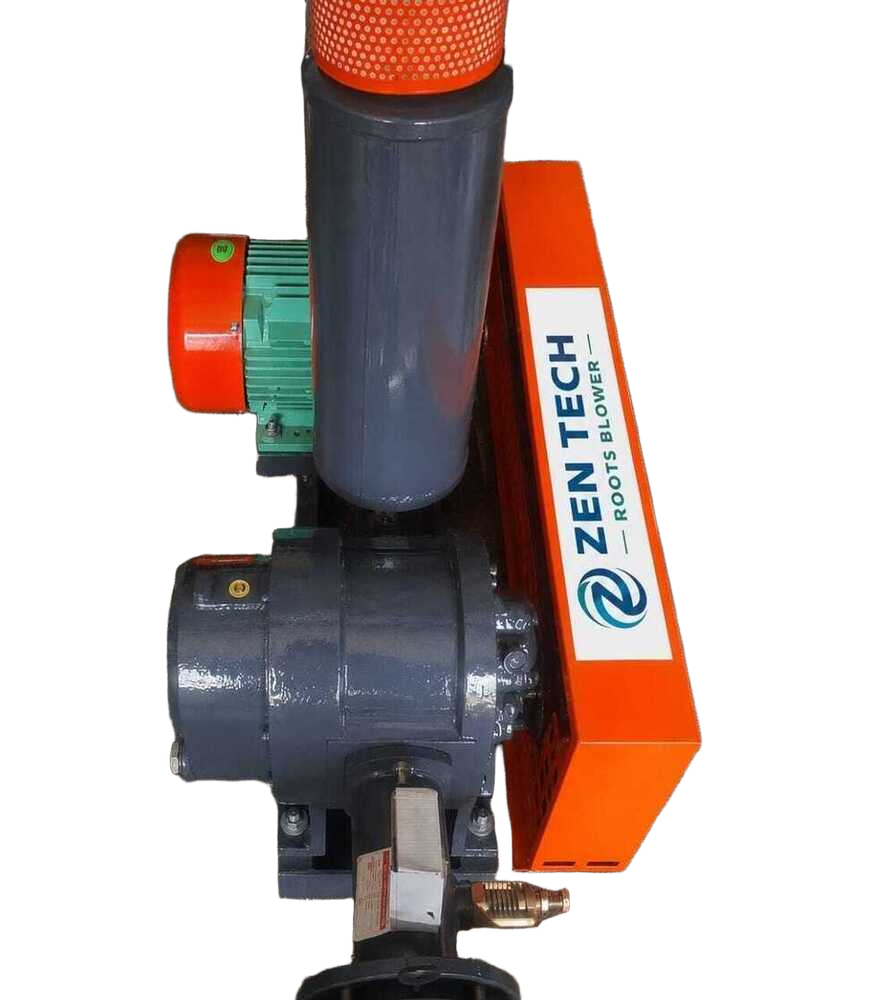
5 HP Roots Air Blower
Price 55000 INR / Unit
Minimum Order Quantity : 1 Unit
Pressure : Other, 0.6 0.8 kg/cm2
Motor Speed : 1440 RPM
Flow Rate : 250450 m3/hr
Vaccum Range : 0.5 to 0.7 kg/cm2
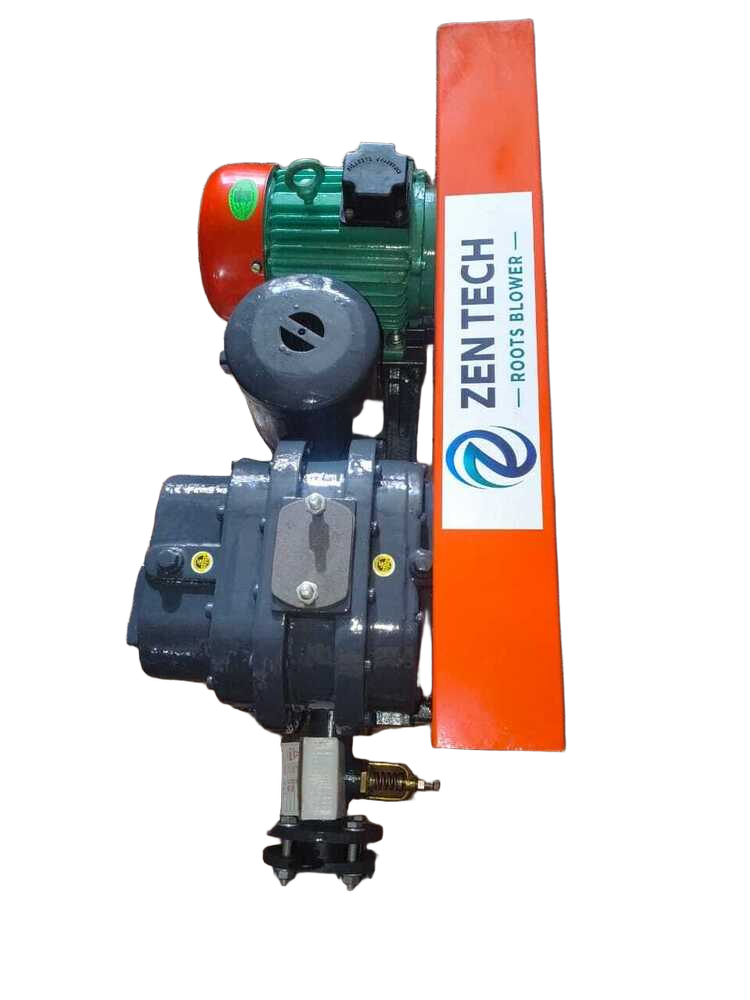
Industrial Twin Lobe Roots Blower
Price 32000 INR / Unit
Minimum Order Quantity : 1 Unit
Pressure : Other, 0.1 to 1 kg/cm2
Motor Speed : 1440 RPM
Flow Rate : 50 to 10,000 m3/hr
Vaccum Range : Up to 500 mmHg
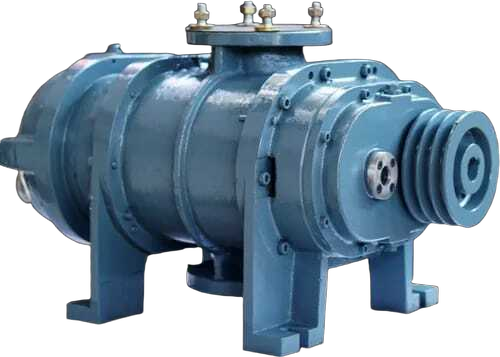
MS Twin Lobe Roots Blower
Minimum Order Quantity : 1 Unit
Pressure : Other, Up to 1 kg/cm2 (G)
Motor Speed : 9602900 RPM
Flow Rate : 50 5000 m3/hr
Vaccum Range : Up to 500 mm Hg (for vacuum models)
STP Twin Lobe Roots Blower
Minimum Order Quantity : 1 Unit
Pressure : Other, 0.35 to 1 kg/cm2
Motor Speed : 1440 RPM
Flow Rate : Up to 7500 m3/hr
Vaccum Range : Up to 500 mm Hg

 Send Inquiry

Plot No. 1, GF, Nizampur Road, Bahadurgarh - 124507, Haryana, India

 Send Inquiry
 Send SMS

Developed and Managed by Infocom Network Private Limited.


